Working Principle of the Material Level Detection Instrument in Grain Steel Silo
With the continuous development of modern technology, grain steel silo are gradually moving towards intelligence. Smart devices are already widely used for real-time monitoring of parameters like temperature and humidity. Likewise, material level detection technology is increasingly being adopted for silo management. With the integration of material level detection, operators can monitor the material levels inside grain steel silos from their office, improving management efficiency. This article will explain the working principle of material level detection instruments in grain steel silos.
Basic Function of the Material Level Detection Instrument
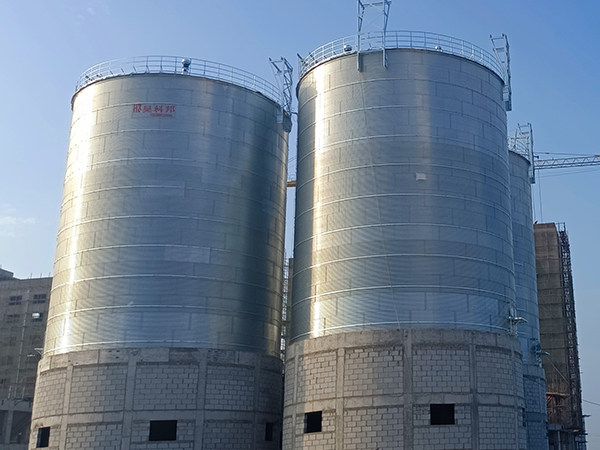
The material level detection instrument is an intelligent device used to monitor the material height inside a grain steel silo in real-time. By using this instrument, operators can view the material levels from a control center or office, eliminating the need for manual checks on top of the silo. This not only improves operational efficiency but also helps avoid safety hazards related to manual operations.
Especially when storing powdery or granular materials, using the material level detection instrument allows real-time monitoring of the material’s condition, ensuring operational safety and accuracy. It plays a crucial role in ensuring smooth operations during the storage process in grain steel silos.
Working Principle of the Heavy Hammer Type Powder Level Meter
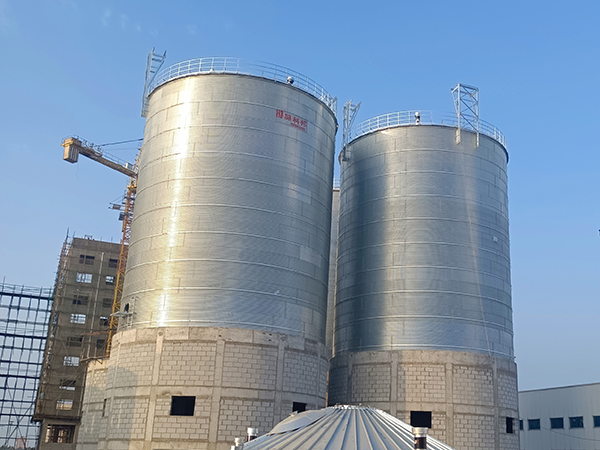
For powdery materials such as cement, fly ash, and mineral powder, the heavy hammer type powder level meter is commonly used for material level detection. This instrument operates based on a servo motor-driven probe that detects material levels from the top of the silo. When the probe touches the material’s surface, the loss of weight in the material triggers a sensor to send an electrical signal. The signal is then processed by a counter and controller, which displays the precise material level.
High Accuracy and Easy Operation
The heavy hammer type powder level meter automatically adjusts the probe’s position during operation, ensuring accurate measurement of the material height. This system offers high measurement accuracy and stability, providing consistent performance even in continuous production processes. Operators only need to view the values through the control system, making it easy to monitor changes in material levels inside the silo.
Additionally, the instrument is highly user-friendly, requiring minimal manual intervention. It typically integrates with the silo’s automation control system, enhancing the level of intelligence in silo management.
Reliability and Durability
The heavy hammer type powder level meter is highly reliable and durable. It can maintain stable performance even in extreme environments, such as high humidity or dusty conditions. As a result, material level monitoring in grain steel silos ensures long-term and stable operation, reducing potential risks caused by equipment failure or inadequate maintenance.
Role of the Material Level Detection Instrument in Grain Storage Management
Grain steel silo are vital for storing grains. The material level detection instrument is an essential part of grain storage management. By continuously monitoring the material levels inside the silo, operators can adjust storage plans in a timely manner. This helps to avoid overfilling or underfilling the silo. Moreover, material level detection can be integrated with temperature and humidity sensors. This integration creates an intelligent monitoring system, enabling more accurate and efficient storage management.
Conclusion
The widespread use of material level detection instruments in grain steel silos has made storage management more intelligent and automated. This has improved the safety and efficiency of grain storage. Through the precise operation of the heavy hammer type powder level meter, operators can obtain accurate material level data in real-time. This reduces the need for manual checks and enhances the monitoring accuracy and safety of the grain storage process. As intelligent technologies continue to progress, the use of material level detection instruments will become more common. This trend will drive the grain storage industry toward greater efficiency and intelligence.