
Grain Silo Conveying System
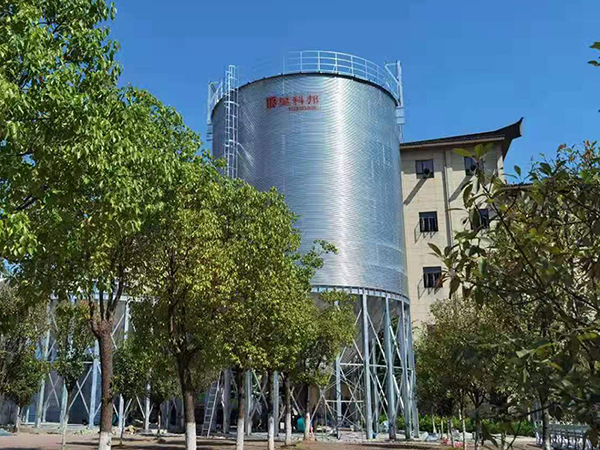
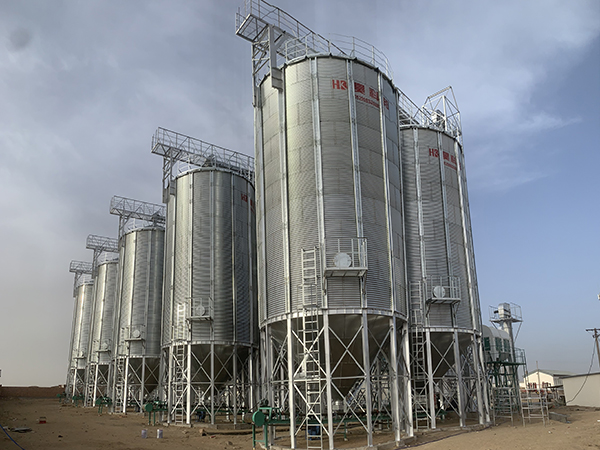
COBAN grain silos are designed to ensure safe storage, stable ventilation, and long-term grain preservation under different climate conditions. Each silo system can be customized based on capacity, grain type, and project requirements for optimal storage performance and reliability.

Grain Silo Conveying System
Application:Grain silos, grain storage facilities, flour mills, rice mills, grain terminals
Conveying Equipment:Bucket elevator, belt conveyor, scraper conveyor, screw conveyor, air-supported conveyor
Capacity Range:20-1000 TPH (Customized according to project requirements)
Conveying Distance:10-300 m (Customized layout design available)
Suitable Materials:Maize, wheat, rice, soybean, barley, sorghum, and other bulk grains
- Customized Capacity Design
- High Strength Galvanized Steel
- ISO Certified Manufacturing
- Global Installation Support
Applications
Corn Storage
Wheat Storage
Rice Storage
Soybean Storage
Feed Storage
Commercial Grain Storage
Product Details & Technical Information
In a modern grain storage project, the silo itself is only one part of the complete system. The efficiency, reliability, and operating cost of a grain storage facility largely depend on the conveying system that connects grain receiving, cleaning, drying, storage, and dispatch processes.
Based on our experience in grain storage projects, we design the grain silo conveying system according to the customer’s actual requirements, including grain type, storage capacity, conveying distance, throughput, site layout, and future expansion plans.
A properly designed grain conveying system should achieve three main goals:
- Maintain stable grain flow during loading and unloading
- Minimize grain damage and contamination
- Reduce dust generation and energy consumption
COBAN provides complete grain handling solutions including bucket elevators, belt conveyors, scraper conveyors, air-supported belt conveyors, screw conveyors, pneumatic conveying systems, and related dust control equipment for grain silos, grain terminals, flour mills, rice mills, and agricultural storage facilities.
What Equipment Is Included in a Complete Grain Silo Conveying System?
A complete grain silo conveying system normally consists of several types of equipment working together:
| Conveying Equipment | Main Function | Typical Application |
|---|---|---|
| Bucket Elevator | Vertical grain lifting | Connecting ground receiving equipment with silo top |
| Belt Conveyor | Horizontal or inclined transportation | Moving grain between silos and processing equipment |
| Scraper Conveyor | Horizontal transportation with multiple discharge points | Grain distribution inside storage facilities |
| Air Supported Belt Conveyor | Long-distance low-loss conveying | Large grain terminals and high-capacity projects |
| Screw Conveyor | Short-distance feeding and discharge | Hopper bottom silos and auxiliary transportation |
| Pneumatic Conveying System | Flexible enclosed grain transfer | Rice, powder materials, and special applications |
| Dust Collection System | Removing airborne dust | Maintaining clean and safe operation |
The correct combination of these machines determines the overall performance of the grain silo handling system.
1. Bucket Elevator for Grain Silo
Vertical Grain Lifting Equipment for High Storage Silos
Bucket elevator is one of the most important machines in a grain silo conveying system. It is mainly used to lift grain vertically from ground level to the top of silos, cleaning machines, dryers, or distribution systems.
In most grain storage projects, the bucket elevator is installed after receiving pits or before the rotary distributor on the silo roof.
Working Principle
The buckets are fixed on a belt or chain and move continuously between the bottom inlet and top discharge section. Grain enters from the bottom, is lifted vertically, and discharged smoothly at the required height.
Main Parameters
| Parameter | Specification |
|---|---|
| Conveying Capacity | 5-800 t/h |
| Lifting Height | 10-60 m |
| Bucket Material | Reinforced nylon / steel |
| Driving Type | Motor + gearbox |
| Grain Damage Rate | ≤0.5% |
| Application | Wheat, maize, rice, soybean, barley |
Advantages
High vertical lifting efficiency
Compared with inclined conveyors, bucket elevators require much less installation space and are ideal for modern high-capacity grain silos.
Stable grain handling
The low-speed bucket design reduces impact during loading and unloading, helping protect grain quality.
Suitable for large silo projects
For projects with silo heights above 20 meters, bucket elevators are usually the most economical solution.
Limitations
- Mainly designed for vertical transportation
- Not suitable for long horizontal conveying distances
- Requires regular inspection of belt tension and bucket wear
Engineering Recommendation
For large grain storage projects:
- 500-5000 tons silo systems usually use standard belt bucket elevators
- Large grain terminals with higher capacity may require heavy-duty chain bucket elevators
- Fragile grains such as rice should use lower-speed elevators to reduce breakage
2. Belt Conveyor for Grain Handling

Reliable Horizontal Grain Transportation Solution
Belt conveyor is widely used in grain silo loading, unloading, and transfer systems because of its simple structure, stable operation, and large conveying capacity.
It is commonly installed:
- Between receiving equipment and bucket elevators
- Between silos
- From dryer outlet to storage silo
- For truck or ship loading systems
Main Parameters
| Parameter | Specification |
|---|---|
| Belt Width | 500-1400 mm |
| Capacity | 50-1000 t/h |
| Conveying Distance | 10-200 m |
| Inclination Angle | ≤18° |
| Belt Speed | 1.0-3.0 m/s |
Different Types of Grain Belt Conveyors
Open Belt Conveyor
Suitable for:
- Outdoor grain transfer
- Short distance conveying
- Large grain storage yards
Advantages:
- Lower investment cost
- Easy maintenance
- Large capacity
Disadvantages:
- More dust exposure
- Requires additional dust control equipment
Enclosed Belt Conveyor
Suitable for:
- Grain terminals
- Flour mills
- Indoor storage facilities
Features:
- Closed dust cover design
- Reduced grain contamination
- Better working environment
Engineering Recommendation
For maize and wheat storage projects in Africa, South America, and Southeast Asia, belt conveyors are usually selected for horizontal grain transportation because they provide a good balance between investment and operating cost.
3. Scraper Conveyor for Grain Storage

Flexible Horizontal Conveying Inside Grain Facilities
Scraper conveyor, also called drag conveyor, uses a chain or scraper flight moving inside a closed trough to transport grain.
It is especially suitable for:
- Grain receiving systems
- Multiple silo distribution lines
- Hopper bottom silo discharge systems
Main Parameters
| Parameter | Specification |
|---|---|
| Capacity | 30-500 t/h |
| Conveying Distance | 20-120 m |
| Installation Angle | Horizontal to 45° |
| Structure | U-shape closed trough |
| Grain Residue | Low residue design |
Advantages
Multiple discharge points
Compared with belt conveyors, scraper conveyors can easily discharge grain at different positions, making them suitable for silo groups.
Fully enclosed structure
The closed design reduces dust leakage and protects grain from external contamination.
Space saving
They can be installed underground or inside steel structures.
Limitations
- Higher power consumption compared with belt conveyors
- More internal wear parts
- Not suitable for extremely long distances
Engineering Recommendation
For a grain storage center with multiple silos, scraper conveyors are often installed under silo outlets to collect and transfer grain efficiently.
4. Air Supported Belt Conveyor
Low Damage and Energy Saving Grain Transportation
Air supported belt conveyor is an advanced solution for large grain terminals and high-capacity storage facilities.
Instead of traditional rollers, the belt floats on an air cushion, reducing friction between belt and support structure.
Main Parameters
| Parameter | Specification |
|---|---|
| Capacity | 100-1500 t/h |
| Belt Width | 800-1600 mm |
| Conveying Distance | 50-300 m |
| Noise Level | <75 dB |
| Energy Saving | Up to 30-35% compared with traditional systems |
Advantages
Extremely low grain damage
The smooth belt movement reduces impact on grain particles.
Lower maintenance requirement
Fewer moving parts mean less mechanical wear.
Suitable for long-distance conveying
It is commonly used in:
- Port grain terminals
- Large grain warehouses
- High-capacity maize storage projects
Limitations
- Higher initial investment
- Requires stable power supply and air system maintenance
Engineering Recommendation
When customers require high throughput, low noise, and continuous operation, air-supported conveyors are usually a better choice than traditional belt conveyors.
5. Screw Conveyor for Grain Silo Discharge

Compact Equipment for Short Distance Transportation
Screw conveyor is commonly used for:
- Hopper bottom silo discharge
- Small storage systems
- Feeding processing equipment
Main Parameters
| Parameter | Specification |
|---|---|
| Capacity | 5-200 t/h |
| Conveying Distance | 3-50 m |
| Installation | Horizontal or inclined |
| Structure | Carbon steel / stainless steel |
Advantages
- Compact structure
- Easy installation
- Good sealing performance
Limitations
- Higher grain friction
- Not recommended for large capacity long-distance transportation
6. Pneumatic Grain Conveying System

Fully Enclosed Solution for Special Applications
Pneumatic conveying uses airflow generated by blowers to transport grain through pipelines.
It is mainly used where traditional mechanical conveyors cannot be installed.
Main Parameters
| Parameter | Specification |
|---|---|
| Conveying Speed | 15-25 m/s |
| Pipeline Type | Stainless steel / carbon steel |
| Working Mode | Positive pressure or negative pressure |
| Application | Rice, seeds, special materials |
Advantages
- Flexible pipeline layout
- Completely enclosed conveying
- Low risk of contamination
Limitations
- Higher energy consumption
- Not suitable for extremely large grain volumes
How to Select the Right Grain Conveyor System?
From our engineering experience, the correct conveying equipment depends on several factors.
1. According to Conveying Distance
| Distance | Recommended Equipment |
|---|---|
| 0-50 m | Belt conveyor / screw conveyor |
| 50-200 m | Belt conveyor / air supported conveyor |
| Vertical lifting | Bucket elevator |
| Multiple discharge points | Scraper conveyor |
2. According to Grain Type
| Grain | Recommended Solution |
|---|---|
| Maize | Bucket elevator + belt conveyor |
| Wheat | Belt conveyor + scraper conveyor |
| Rice | Low-speed elevator + pneumatic conveying |
| Soybean | Scraper conveyor + enclosed conveyor |
| Seed grain | Low-damage conveying system |
3. According to Project Capacity
Small Grain Storage Project
Recommended:
- Bucket elevator
- Screw conveyor
- Small belt conveyor
Capacity:
50-500 tons/day
Medium Grain Storage Center
Recommended:
- Bucket elevator
- Belt conveyor
- Scraper conveyor
- Dust collection system
Capacity:
500-3000 tons/day
Large Grain Terminal
Recommended:
- High-capacity bucket elevator
- Air-supported belt conveyor
- Automatic control system
- Intelligent monitoring system
Capacity:
3000+ tons/day
COBAN Grain Silo Conveying System Design
Every grain storage project has different requirements. A standard conveyor layout cannot achieve the best performance for every customer.
Our engineering team designs the complete grain silo conveying system based on:
- Grain type and characteristics
- Required throughput
- Storage capacity
- Site layout
- Loading and unloading process
- Future expansion requirements
A complete COBAN grain handling system can integrate:
✓ Receiving system
✓ Cleaning system
✓ Drying system
✓ Grain silo storage
✓ Conveying equipment
✓ Dust collection system
✓ Automatic control system
Through reasonable equipment selection and layout design, customers can achieve higher efficiency, lower operating costs, and safer grain storage operation.
Build Your Grain Silo Conveying Solution with COBAN
Whether you are planning a new grain storage facility, expanding an existing silo project, or upgrading your grain handling system, COBAN can provide a complete conveying solution according to your actual production requirements.
Contact our engineering team to discuss your grain silo conveying system design, equipment selection, and project configuration.
Request A Quote
Tell us your capacity, grain type, and project location. We will design a turnkey solution for you.